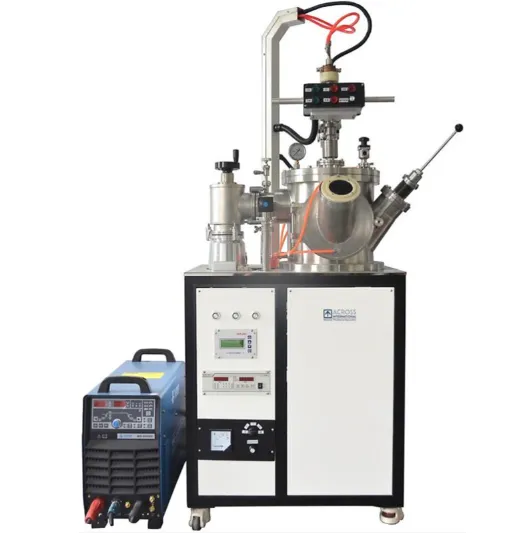

The AIVAF metal melting furnace stands as a compact arc melting furnace, adept at transforming alloy ingots through multiple smelting cycles while preserving the controlled atmosphere intact. It facilitates the preparation of numerous samples concurrently, making it an optimal apparatus for universities and research institutes engaged in the creation of refractory metal and metal carbide samples.

The Ai AIVAF Vacuum Arc Melting Furnace is a high-performance laboratory system designed for melting, alloying and preparation of refractory metals, specialty alloys and advanced metallic materials.
Capable of reaching temperatures up to 3500°C, the AIVAF combines high-current arc melting with a high-vacuum molecular pumping system, water-cooled copper hearth, electromagnetic stirring and vacuum suction casting. The system achieves an ultimate chamber vacuum down to 6.67 × 10⁻⁴ Pa, providing a clean and controlled environment for materials that are sensitive to oxidation and contamination.
Advanced Arc Melting System
The system uses a tungsten electrode with high-frequency arc ignition to generate the intense heat required for melting high-melting-point materials. Two configurations are available:
AF-50: up to 500 A
AF-70: up to 1200 A
The vacuum chamber is double-layer water cooled to protect the chamber and critical components during high-temperature operation.
5-Position Water-Cooled Copper Hearth
The AIVAF features a five-position water-cooled copper hearth, allowing different samples and processing steps to be performed within the same vacuum chamber.
The hearth includes:
3 alloy melting positions with electromagnetic stirring
1 ingot / suction casting position
1 degassing melting position
Electromagnetic stirring promotes movement of the molten material, helping improve mixing and compositional uniformity during alloy preparation.
Repeated Melting Under Controlled Atmosphere
An integrated manipulator allows the operator to flip and re-melt alloy samples inside the vacuum chamber. Multiple melting cycles can therefore be performed without opening the chamber, helping improve alloy homogeneity while reducing exposure to air.
The system supports controlled processing using high-purity argon (Ar), helium (He), or 5% H₂ / 95% Ar protective atmospheres.
Integrated Vacuum Suction Casting
A dedicated vacuum suction casting system allows molten alloy samples to be rapidly transferred into a compatible mould. This makes the AIVAF suitable not only for alloy melting, but also for small-scale casting and advanced materials development.
High Vacuum System
The integrated mechanical and turbo molecular pumping system provides:
Ultimate chamber vacuum: 6.67 × 10⁻⁴ Pa
Turbo pumping speed: 300 L/s (AF-50) or 600 L/s (AF-70)
Pump-down performance: ≤5 × 10⁻³ Pa within 30 minutes
Vacuum measurement range: 10⁻⁵ to 10⁵ Pa
Key Features
Maximum melting temperature up to 3500°C
500 A or 1200 A arc melting configurations
High vacuum down to 6.67 × 10⁻⁴ Pa
5-position water-cooled copper hearth
3 electromagnetic stirring positions
In-chamber sample flipping and repeated melting
Integrated vacuum suction casting
Double-layer water-cooled stainless steel chamber
Controlled Ar, He and Ar/H₂ atmospheres
Maximum sample capacity up to 157 g (AF-50) or 408 g (AF-70) per position, based on iron
Ideal for refractory metals, high-entropy alloys, specialty alloys and advanced materials research
Typical Applications
The AIVAF is ideal for universities, research institutes and advanced materials laboratories working with refractory metals, high-entropy alloys (HEAs), titanium alloys, nickel- and cobalt-based alloys, intermetallic compounds, metal carbides and other specialised alloy systems.
Its combination of high-temperature arc melting, high vacuum, electromagnetic stirring, repeated re-melting and suction casting provides a versatile platform for alloy development, materials research and small-scale sample preparation.
| Product Name | Picture |
| AI-AF Vacuum Arc Furnace |  |
| Copper crucibles | 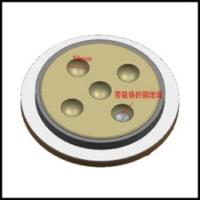 |
| Vacuum suction casting device |   |
| Lighting LED lights |  |
| Chamber door |  |
| Observation window |  |
| Electromagnetic stirring |  |
Tungsten electrode |  |
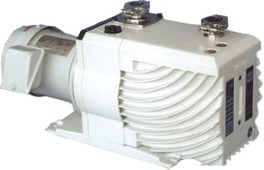
Mechanical Pump |  |
Large high vacuum manual baffle valve |  |
Composite vacuum gauge |  |
Molecular pump unit |  |